
Stainless Steel Vortex Magnetic Pump for Efficient Fluid Handling
By:Admin
Company News & Blog
Learn about the benefits of single stage centrifugal pumps for your business
Single Stage Centrifugal Pump Revolutionizes the Pumping IndustryThe pumping industry has seen a revolutionary change with the introduction of the Single Stage Centrifugal Pump by a leading company in the field. This state-of-the-art pump is designed to meet the demanding requirements of various industries and has set new benchmarks in terms of performance, efficiency, and reliability.This innovative pump is the result of years of research and development by the company's team of experts. It combines advanced engineering techniques with cutting-edge technology to deliver an unparalleled pumping solution. The pump is capable of handling a wide range of fluids and is suitable for applications in industries such as chemical processing, water treatment, power generation, and more.One of the key features of the Single Stage Centrifugal Pump is its high efficiency, which leads to significant energy savings for the end user. This is achieved through a combination of precision engineering and the use of premium quality materials, which ensure minimal friction and maximum output. The pump also boasts a robust construction, which enhances its durability and longevity, making it a cost-effective investment for any business.In addition to its high efficiency, the Single Stage Centrifugal Pump also offers unparalleled performance. It is capable of delivering a consistent flow and pressure, ensuring smooth and reliable operation. This makes it an ideal choice for critical applications where precision and consistency are paramount.Furthermore, the pump is designed for easy installation and maintenance, reducing downtime and lowering the total cost of ownership for the end user. Its user-friendly design and intuitive controls make it easy to operate, while its modular construction allows for quick and hassle-free servicing.The company behind this groundbreaking pump is a leading player in the pumping industry, with a rich legacy of innovation and excellence. Established decades ago, the company has earned a reputation for delivering high-quality pumping solutions that meet the evolving needs of various industries.With a strong focus on research and development, the company invests heavily in cutting-edge technologies and engineering capabilities. This has enabled it to develop a wide range of pumps that are known for their superior performance, reliability, and durability. The company's commitment to excellence is reflected in its stringent quality control measures and adherence to international standards.Moreover, the company prides itself on its customer-centric approach, offering comprehensive support and service to its clients. Its team of experienced engineers and technicians are dedicated to providing expert guidance and assistance, ensuring that customers get the most out of their pumping solutions.The introduction of the Single Stage Centrifugal Pump is a testament to the company's commitment to innovation and its dedication to meeting the evolving needs of the industry. With its unmatched performance, efficiency, and reliability, this pump is set to revolutionize the pumping industry and set new standards for years to come.In conclusion, the Single Stage Centrifugal Pump by the leading company is a game-changer in the pumping industry. With its cutting-edge design, advanced features, and superior performance, it has raised the bar for pumping solutions and has the potential to transform various industries. As the company continues to push the boundaries of engineering and technology, we can expect to see more groundbreaking innovations that will further solidify its position as a leader in the field.
Top Quality Immersible Pump Factory Offers Advanced Pumping Solutions
Fy Immersible Pump Factory, located in the heart of the industrial district, has been a leading manufacturer and supplier of high-quality immersible pumps for various industries for over two decades. The factory prides itself on its state-of-the-art production facilities and a team of highly skilled engineers and technicians dedicated to ensuring the highest standards of quality and performance.The factory specializes in the design and production of immersible pumps for applications such as water supply, wastewater treatment, industrial processes, and many others. With a focus on innovation and continuous improvement, Fy Immersible Pump Factory has built a solid reputation for delivering reliable and efficient pumping solutions to its customers worldwide.In recent news, the factory has announced its latest product line, featuring advanced technologies and enhanced performance capabilities. This new line of immersible pumps is designed to meet the growing demand for more efficient and reliable pumping solutions in various industries.One of the key highlights of the new product line is its innovative design that offers improved energy efficiency and lower operating costs. The factory's engineering team has incorporated cutting-edge technologies to optimize the hydraulic and mechanical performance of the pumps, resulting in significant energy savings for the end-users.Furthermore, the new product line also features enhanced durability and reliability, making it ideal for demanding industrial applications. The factory has employed rigorous testing and quality control measures to ensure that each pump meets the highest standards of performance and reliability, even in the most challenging operating conditions."We are excited to introduce our latest product line of immersible pumps, which represents a significant leap forward in terms of performance, efficiency, and reliability," said the spokesperson of Fy Immersible Pump Factory. "We have invested heavily in research and development to bring these innovative solutions to the market, and we are confident that they will set a new standard for immersible pumping technology."The factory has also emphasized its commitment to sustainability by incorporating eco-friendly design elements and materials in the new product line. With a focus on reducing environmental impact, the factory aims to provide pumping solutions that not only deliver superior performance but also contribute to a more sustainable and greener future.In addition to the launch of the new product line, Fy Immersible Pump Factory has also expanded its global distribution network to better serve its customers in various regions. The factory has partnered with reputable distributors and service providers to ensure timely delivery, installation, and after-sales support for its products, further solidifying its position as a trusted partner for pumping solutions.As the demand for reliable and efficient immersible pumps continues to grow across industries, Fy Immersible Pump Factory remains at the forefront of innovation and technological advancement. With its latest product line and expanded distribution network, the factory is well-positioned to meet the evolving needs of its customers and provide cutting-edge pumping solutions for a wide range of applications.In conclusion, Fy Immersible Pump Factory's latest announcement reflects its ongoing commitment to delivering high-quality, efficient, and sustainable pumping solutions to its global customer base. With a focus on innovation, performance, and reliability, the factory is poised to set new industry standards and continue its legacy as a leading manufacturer of immersible pumps.Overall, Fy Immersible Pump Factory's dedication to excellence and its continuous pursuit of technological advancement position it as a key player in the global market for pumping solutions, and the latest product line launch only further solidifies its standing in the industry.
Double Helical Gear Pump: Features, Benefits, and Applications
Certainly! Please provide the news content about the Double Helical Gear Pump (without the brand name) and the company introduction you’d like included. Once I have those details, I can help craft an 800-word news article for you.
Top Sewage Pump Manufacturers | Reliable Sewage Pump Suppliers
Certainly! Please provide the company introduction and the news content (with the brand name removed), so I can craft the 800-word news article for you.
Self Priming Centrifugal Oil Pump: Features and Benefits
Certainly! Please provide the news content about the Self Priming Centrifugal Oil Pump and the company introduction you would like me to use.
Corrosion Resistant Vacuum Pump Manufacturer | High-Quality Durable Vacuum Pumps
Certainly! Please provide the specific news content and the company introduction you want me to use (excluding the brand name), and I will draft an 800-word news article accordingly.
High-Quality Belt Gear Pumps for Efficient Fluid Transfer
Certainly! Please provide the specific news content about the Belt Gear Pump and the company introduction {} so I can craft the 800-word news article for you.
Efficient Axial Flow Pump for Chemical Applications
Harizontal Chemical Axial Flow Pump: The Ideal Solution for Heavy Duty Industrial ApplicationsThe industrial sector relies on a range of heavy-duty equipment to ensure smooth and efficient operations. Among these, the Harizontal Chemical Axial Flow Pump has emerged as a reliable and high-performance solution for the pumping needs of various industrial processes. With its advanced technology and innovative design, this pump has become an essential component in industries such as chemical processing, water treatment, and mining.The Harizontal Chemical Axial Flow Pump, manufactured by a leading global company specializing in fluid handling solutions, is designed to meet the most rigorous demands of industrial applications. With its robust construction and high efficiency, this pump is capable of handling corrosive and abrasive fluids, making it an ideal choice for challenging environments.One of the key features of the Harizontal Chemical Axial Flow Pump is its axial flow design, which allows for the smooth and efficient movement of fluids. Unlike traditional centrifugal pumps, which rely on impeller rotation to generate fluid flow, axial flow pumps use a propeller-like impeller to create a linear flow pattern. This design not only enables the pump to operate at higher flow rates but also results in lower energy consumption, making it a cost-effective solution for industrial operations.The Harizontal Chemical Axial Flow Pump is also known for its versatility, as it can handle a wide range of fluids, including chemicals, slurries, and wastewater. This broad application range makes it a valuable asset for industries that deal with diverse fluid handling requirements. Whether it is transferring corrosive chemicals in a manufacturing plant or managing water circulation in a municipal facility, this pump delivers consistent and reliable performance.In addition to its exceptional performance, the Harizontal Chemical Axial Flow Pump is also engineered for durability and minimal maintenance. The pump's design incorporates high-quality materials and components, ensuring long-term reliability even in harsh operating conditions. Furthermore, the pump's streamlined configuration and straightforward maintenance procedures translate to reduced downtime and lower lifecycle costs for industrial operations.As a global leader in fluid handling solutions, the company behind the Harizontal Chemical Axial Flow Pump has a proven track record of delivering innovative and reliable products to the industrial market. With a strong focus on research and development, the company continues to enhance its product offerings to address the evolving needs of the industry. Furthermore, its commitment to quality and customer satisfaction has earned it a reputation for excellence in the field of fluid handling equipment.The Harizontal Chemical Axial Flow Pump represents the company's dedication to providing cutting-edge solutions for industrial fluid handling challenges. By leveraging advanced engineering techniques and extensive industry expertise, the company has developed a pump that sets new standards for performance, reliability, and efficiency. Additionally, the company's comprehensive support services ensure that customers receive tailored solutions and responsive assistance for their specific applications.In conclusion, the Harizontal Chemical Axial Flow Pump stands as a testament to the advancements in fluid handling technology, offering a robust and efficient solution for industrial pumping requirements. With its axial flow design, versatile capabilities, and exceptional durability, this pump is well-suited for the demanding needs of chemical processing, water treatment, and mining operations. Backed by the expertise and commitment of a leading global company, the Harizontal Chemical Axial Flow Pump exemplifies the future of industrial pumping solutions.
High Performance Close Coupled Centrifugal Pump for Efficient Water Movement
[Company Name] Introduces Cutting-Edge Close Coupled Centrifugal Pump[Company Name], a leading provider of industrial equipment, has recently introduced a new close coupled centrifugal pump that is set to revolutionize the pumping industry. The company, known for its innovative and high-quality products, has designed this pump to meet the highest standards of performance, reliability, and efficiency.The close coupled centrifugal pump is a key addition to [Company Name]'s extensive line of industrial pumps and equipment. It is designed to handle a wide range of pumping applications, including water circulation, chillers, air conditioning systems, and heating systems. With its compact design and high-efficiency performance, the pump is ideal for a variety of commercial and industrial settings.One of the key features of the close coupled centrifugal pump is its space-saving design. The pump is mounted directly onto the motor, eliminating the need for a separate baseplate and coupling. This not only reduces installation time and costs but also makes it easier to maintain and service the pump. The compact design also makes the pump suitable for applications where space is limited, such as in small mechanical rooms or equipment enclosures.In addition to its space-saving design, the close coupled centrifugal pump offers excellent performance and reliability. It is equipped with a high-efficiency motor and impeller, which ensure smooth and efficient operation. The pump is also constructed with high-quality materials that are resistant to corrosion and wear, ensuring long-term durability and performance.Furthermore, the pump is designed for easy maintenance and service. Its simple and accessible design allows for quick and easy access to internal components, reducing downtime and maintenance costs. This makes the pump an ideal choice for facilities that require reliable and efficient pumping solutions.[Company Name] is known for its commitment to quality and innovation, and the introduction of the close coupled centrifugal pump is a testament to this. The company's team of engineers and designers have worked tirelessly to develop a pump that meets the highest standards of performance and reliability. With its cutting-edge technology and advanced design, the pump is poised to become a game-changer in the pumping industry.The close coupled centrifugal pump is the latest addition to [Company Name]'s comprehensive range of industrial equipment. The company offers a wide range of pumps, motors, and accessories, designed to meet the diverse needs of its customers. From small-scale commercial applications to large industrial projects, [Company Name] provides solutions that are efficient, reliable, and cost-effective.With the introduction of the close coupled centrifugal pump, [Company Name] continues to demonstrate its commitment to providing innovative and high-quality industrial equipment. The company's dedication to excellence and customer satisfaction has made it a trusted partner for businesses across various industries. As the pumping industry continues to evolve, [Company Name] remains at the forefront, delivering cutting-edge solutions that meet the needs of modern businesses.In conclusion, the introduction of the close coupled centrifugal pump signifies [Company Name]'s dedication to innovation and excellence in the pumping industry. With its space-saving design, high performance, and reliability, the pump is poised to set new standards for industrial pumping solutions. As [Company Name] continues to push the boundaries of technology and design, businesses can rely on the company to provide advanced, efficient, and reliable industrial equipment for their operations.
Benefits of Using a Water Ring Vacuum Pump
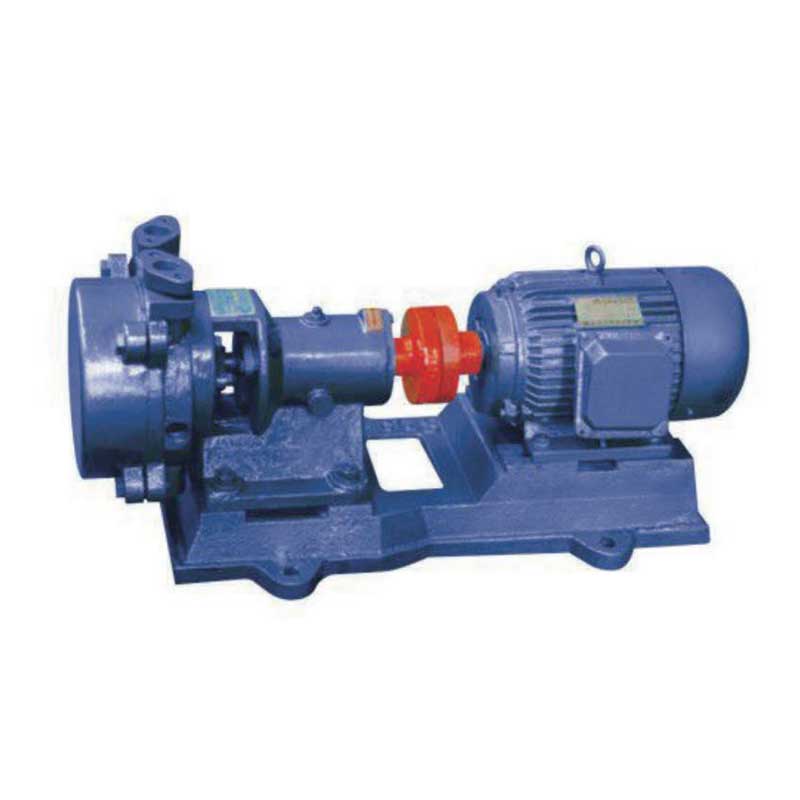
Title: Innovative Water Ring Vacuum Pump Technology Revolutionizing Industrial Applications Introduction:In a bid to enhance industrial efficiency and sustainability, a pioneering company has recently developed an advanced Water Ring Vacuum Pump. This groundbreaking technology promises to revolutionize various industrial processes, offering improved performance, reduced energy consumption, and more eco-friendly operations.Company Introduction:With a strong commitment to innovation and a focus on delivering cutting-edge solutions, Company X has emerged as a leader in the field of industrial machinery technology. Since its inception, the company has consistently developed and introduced state-of-the-art equipment to address the evolving needs of industries worldwide.The New Generation Water Ring Vacuum Pump:Addressing the demand for a more efficient vacuum pump system, Company X presents its latest development: the New Generation Water Ring Vacuum Pump (abbreviated as NGWRVP). This pump utilizes advanced engineering and pioneering design principles, ensuring outstanding performance across a multitude of industrial applications.Features and Benefits:1. Enhanced Performance: The NGWRVP offers superior performance compared to conventional models, boasting a higher volumetric efficiency and excellent suction capacity. These improvements result in faster evacuation times and increased productivity for industries, minimizing downtime and optimizing overall efficiency.2. Energy Efficiency: By leveraging innovative design concepts, the NGWRVP significantly reduces energy consumption. With a carefully balanced construction and improved internal components, the pump achieves optimized power utilization, leading to substantial energy savings for industrial operations.3. Reduced Environmental Impact: Recognizing the importance of sustainability, Company X has engineered the NGWRVP to have a minimal environmental footprint. By reducing energy consumption, the new pump helps lower greenhouse gas emissions, contributing to a greener industrial sector.4. Durability and Reliability: Built to withstand demanding operational conditions, the NGWRVP features a robust and corrosion-resistant design. Its enhanced durability ensures a longer operational lifespan, minimizing the need for frequent replacements and reducing maintenance costs for industries.Applications:The NGWRVP boasts a versatile application range, making it suitable for a broad spectrum of industries. Some key areas where this innovative pump can significantly enhance operations include:1. Chemical Processing: From evaporators to distillation columns and reactors, the NGWRVP facilitates efficient vacuum applications, ensuring optimized chemical processing and reducing energy waste.2. Pharmaceutical Industry: Vacuum applications play a fundamental role in pharmaceutical manufacturing. The NGWRVP provides precise vacuum control, contributing to the production of high-quality pharmaceutical products while keeping energy consumption in check.3. Food Processing: In food industries, the NGWRVP excels in deaeration, filtration, and drying processes. Its ability to handle condensable and non-condensable gases efficiently ensures enhanced quality and safety standards for food products.4. Manufacturing: From automotive to aerospace industries, the NGWRVP enables improved performance in various manufacturing processes such as molding, brazing, and packaging, resulting in higher productivity and operational excellence.Conclusion:The introduction of Company X's New Generation Water Ring Vacuum Pump exemplifies their commitment to pioneering innovation and sustainable solutions for industrial applications. With its enhanced performance, energy efficiency, and reduced environmental impact, this groundbreaking technology is set to revolutionize diverse industries, paving the way for a more efficient and eco-friendly manufacturing landscape.