
Multistage Centrifugal Pump: Features, Applications, and Benefits
By:Admin
Company News & Blog
Top 5 High-Performance Chemical Pumps for Industrial Use
Chemical Pump is a leading provider of high-quality pumps and pumping solutions for a wide range of industries. With a strong commitment to innovation and customer satisfaction, the company has established itself as a trusted partner for businesses seeking reliable and efficient pumping equipment.The company's extensive product range includes chemical pumps, centrifugal pumps, and other industrial pump solutions, all of which are designed to meet the specific needs of their customers. Chemical Pump's dedication to quality and performance is reflected in their products, which are built to withstand the most demanding operating conditions.One of the key factors that sets Chemical Pump apart from its competitors is its focus on research and development. The company's team of engineers and technical experts are constantly striving to improve and enhance their product offerings, ensuring that they remain at the forefront of technological advancement in the industry.In addition to its commitment to innovation, Chemical Pump is also dedicated to providing exceptional customer service. The company works closely with its clients to understand their unique requirements and provide tailored pumping solutions that meet their specific needs. Whether it's a small-scale operation or a large industrial facility, Chemical Pump has the expertise and resources to deliver reliable and cost-effective pumping solutions.Furthermore, the company takes great pride in its responsible and sustainable business practices. Chemical Pump is committed to minimizing its environmental impact and promoting energy efficiency in all aspects of its operations. By investing in advanced technologies and manufacturing processes, the company strives to reduce waste and conserve resources, while also ensuring the safety and well-being of its employees and the communities in which it operates.Chemical Pump's dedication to excellence has earned it a solid reputation in the industry, and the company continues to be a preferred choice for businesses seeking high-quality pumping solutions. With a global presence and a strong network of distributors, Chemical Pump is well-positioned to serve customers around the world.In conclusion, Chemical Pump is a company that is dedicated to delivering high-quality pumping solutions for a wide range of industries. With its focus on innovation, customer service, and sustainability, the company has established itself as a trusted partner for businesses seeking reliable and efficient pumping equipment. Whether it's for chemical processing, water treatment, or other industrial applications, Chemical Pump has the expertise and resources to meet the unique needs of its customers.
Explore the Benefits of Single Stage Single Suction Chemical Pumps
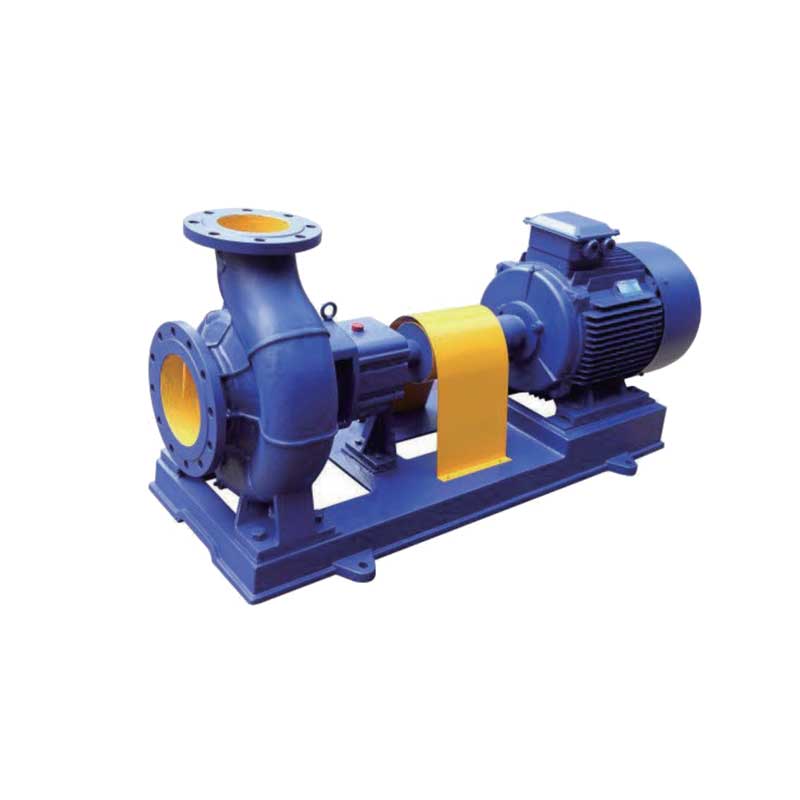
We are excited to introduce the latest addition to our product line, the Single Stage Single Suction Chemical Pumps. As a leading manufacturer of industrial pumps, we are constantly striving to innovate and provide high-quality solutions to our customers in the chemical processing industry.Our company has been in the business for over 20 years and has established a strong reputation for reliability and performance. We understand the unique challenges that our customers face when it comes to handling corrosive and toxic chemicals, and we are committed to developing pumps that can meet these demands.The Single Stage Single Suction Chemical Pumps are designed to handle a wide range of chemicals, including acids, alkalis, and solvents. With a compact and efficient design, these pumps offer reliable performance and low maintenance, making them an ideal choice for critical chemical processing applications.One of the key features of our Single Stage Single Suction Chemical Pumps is their corrosion resistance. These pumps are constructed with materials that can withstand the harsh conditions of chemical processing, ensuring long-term reliability and performance. Additionally, the pumps are designed for easy installation and operation, allowing our customers to streamline their processes and improve productivity.In addition to their technical capabilities, our Single Stage Single Suction Chemical Pumps also prioritize safety. We understand the importance of maintaining a safe working environment when dealing with hazardous chemicals, and our pumps are designed with various safety features to minimize the risk of leaks and spills.Furthermore, our company is committed to providing comprehensive support to our customers, and our team of experienced engineers and technicians are available to provide technical assistance and maintenance services for the Single Stage Single Suction Chemical Pumps. We strive to build long-lasting relationships with our customers and ensure that they get the most out of our products.The introduction of the Single Stage Single Suction Chemical Pumps reflects our ongoing commitment to innovation and customer satisfaction. We are confident that these pumps will provide our customers with the reliable and efficient solution they need for their chemical processing applications.In conclusion, the Single Stage Single Suction Chemical Pumps represent a significant advancement in our product line, and we are excited to bring this new offering to our customers in the chemical processing industry. With their robust construction, corrosion resistance, and focus on safety, these pumps are designed to meet the demanding requirements of handling various chemicals. As a company, we are dedicated to providing high-quality solutions and exceptional support to our customers, and we believe that the Single Stage Single Suction Chemical Pumps will further strengthen our position as a trusted partner in the industry.
High-Efficiency Vacuum Discharge Pump for Industrial Applications
Certainly! Please provide the news content about the Vacuum Discharge Pump as well as the company introduction {} so I can create the 800-word news article for you.
Single Stage Single Suction Chemical Pump for Efficient Fluid Handling
Certainly! Please provide the specific news content about the Single Stage Single Suction Chemical Pump and the company introduction you would like me to use. Once I have those details, I can draft an 800-word news article for you.
Highly Efficient Flow Evaporating Circulating Pump for Improved Performance
Flow Evaporating Circulating Pump Revolutionizes Industrial ProcessesIndustrial processes often require the circulation of liquid or gas to cool, transfer heat, or maintain the right chemical balance. Traditionally, this has involved the use of traditional pumps that can be inefficient, prone to damage, and costly to maintain. However, thanks to the innovative technology of the Flow Evaporating Circulating Pump, these issues can be a thing of the past.The Flow Evaporating Circulating Pump, developed by a leading company in fluid handling and heat transfer solutions, is a game-changer in the industrial pump market. It represents a significant advancement in pump technology, offering superior performance, energy efficiency, and reliability compared to traditional pumps.This revolutionary pump is specifically designed for applications where the circulating fluid undergoes phase change, such as evaporation and condensation. It is ideal for use in industries such as chemical processing, power generation, food and beverage production, and HVAC systems, where precise temperature control and efficient heat transfer are critical.The Flow Evaporating Circulating Pump operates on the principle of evaporation-induced flow, which allows for increased heat transfer rates and improved energy efficiency. This unique design minimizes the risk of cavitation and ensures smooth, continuous operation, even under demanding conditions.One of the key advantages of this innovative pump is its ability to handle a wide range of fluid types, including corrosive, viscous, and abrasive fluids. This versatility makes it suitable for a variety of industrial applications, providing a cost-effective and reliable solution for fluid circulation and heat transfer.In addition to its impressive performance capabilities, the Flow Evaporating Circulating Pump is also designed with ease of maintenance in mind. Its robust construction and advanced materials ensure long-lasting durability, while its simple and intuitive design allows for easy access to critical components for routine servicing and repairs.Furthermore, the pump is equipped with advanced monitoring and control features, allowing operators to optimize its performance and troubleshoot any issues quickly. This not only helps to minimize downtime and maintenance costs but also ensures that the pump operates at peak efficiency at all times.The company behind the Flow Evaporating Circulating Pump has a proven track record of delivering innovative fluid handling solutions to a global customer base. With a commitment to continuous research and development, they have established themselves as a leader in the field, providing cutting-edge products that address the evolving needs of industry.In addition to their technical expertise, the company places a strong emphasis on customer satisfaction, offering comprehensive support services and technical assistance to ensure that their products meet and exceed customer expectations. This dedication to excellence has earned them a reputation for reliability, quality, and innovation in the fluid handling industry.As industry demands for more efficient and reliable fluid handling solutions continue to grow, the Flow Evaporating Circulating Pump stands out as a game-changing technology that is poised to revolutionize industrial processes. With its advanced design, superior performance, and ease of maintenance, this innovative pump offers a compelling value proposition for a wide range of applications across diverse industries.In conclusion, the Flow Evaporating Circulating Pump represents a significant leap forward in pump technology, offering a compelling alternative to traditional pumps for industrial fluid handling and heat transfer applications. With its innovative design, superior performance, and commitment to reliability, it has the potential to transform the way industrial processes are managed and optimized.
Magnetic Drive Pump: Key Features and Applications Explained
**Innovative Magnetic Drive Pump Enhances Industrial Efficiency and Safety**In the rapidly evolving landscape of industrial technology, equipment that combines reliability, efficiency, and environmental safety is in high demand. Among the latest advancements capturing attention is the Magnetic Drive Pump, a cutting-edge solution engineered to meet the challenges of modern industrial operations. This innovative pump design promises to optimize performance while minimizing maintenance and potential hazards associated with traditional pump systems.**Revolutionizing Pump Technology**The Magnetic Drive Pump distinguishes itself through a unique, seal-less structure that eliminates the need for conventional shaft seals. By employing a powerful magnetic coupling mechanism, the pump transfers torque from the motor to the impeller without direct mechanical contact. This design significantly reduces the risk of leaks, a common issue that can lead to costly downtime, environmental contamination, and safety concerns in industries handling hazardous or corrosive fluids.With its hermetically sealed construction, the Magnetic Drive Pump offers superior containment of liquids, making it particularly suitable for chemical processing, pharmaceuticals, petrochemicals, and wastewater treatment plants. The absence of dynamic seals also means decreased wear and tear, translating into longer service intervals and reduced maintenance costs for operators.**Key Features and Benefits**- **Leak-Proof Operation:** The magnetically coupled drive eliminates potential leak paths, safeguarding the environment and workplace from exposure to harmful substances. - **Enhanced Durability:** Stainless steel and other corrosion-resistant materials used in constructing the pump body and magnetic components extend operational life, even under harsh conditions. - **Energy Efficiency:** Precisely engineered magnetic couplings minimize energy loss, contributing to lower electricity consumption and operational expenses. - **Quiet and Smooth Performance:** The magnetic drive mechanism operates with less vibration and noise compared to traditional pumps, improving working conditions. - **Versatile Applications:** Its robust design allows for handling a wide range of fluids, including aggressive chemicals, solvents, and slurry mixtures, catering to diverse industrial needs.**Company’s Commitment to Innovation and Quality**Behind this breakthrough is a company renowned for its dedication to delivering high-quality industrial equipment that meets stringent international standards. With decades of experience specializing in fluid machinery, this company has established a reputation for innovation, reliability, and customer-centric service. Its product portfolio encompasses a broad spectrum of pumps and related solutions designed to drive efficiency and sustainability across various sectors.Leveraging state-of-the-art research and development facilities, the company continuously refines its Magnetic Drive Pump technology to adapt to changing market demands and regulatory requirements. Strategic collaborations with global partners ensure the integration of best practices and cutting-edge materials, reinforcing the pump’s position as a market leader.Additionally, comprehensive after-sales support and technical consultation services provided by the company empower clients to maximize the performance and longevity of their equipment. Training programs and customized maintenance plans further exemplify the company’s holistic approach to fostering long-term partnerships.**Sustainability and Environmental Impact**In alignment with global initiatives focusing on sustainable industrial practices, the Magnetic Drive Pump contributes significantly to reducing environmental footprints. By preventing leaks and minimizing emissions of volatile organic compounds (VOCs), the pump aids companies in complying with environmental regulations and corporate social responsibility goals.Moreover, its high efficiency reduces power consumption, which not only lowers operational costs but also helps decrease greenhouse gas emissions associated with energy generation. The durability and reliability of the pump also diminish the frequency of replacements and repairs, thereby reducing waste and resource use.**Market Outlook and Industry Adoption**Market analysts observe a growing trend toward adopting magnetic drive pumps in sectors where safety and fluid containment are paramount. As industries increasingly prioritize automation, environmental safety, and cost reduction, the demand for advanced pump solutions like this one continues to rise.Early adopters in chemical manufacturing, pharmaceutical production, and water treatment have reported noticeable improvements in operational stability and maintenance cycles. Case studies highlight successful integration into complex systems, demonstrating the pump’s compatibility with existing infrastructure and process requirements.**Conclusion**The Magnetic Drive Pump represents a significant advancement in industrial fluid handling technology, offering a blend of safety, efficiency, and durability that meets the rigorous demands of today’s industries. Supported by a company with a strong heritage of innovation and customer support, this pump is poised to become an indispensable component in sectors striving for operational excellence and environmental stewardship.As industries navigate the challenges of modern production and sustainable development, embracing technologies such as the Magnetic Drive Pump will be crucial in achieving both economic and ecological goals. Stakeholders looking for reliable, state-of-the-art pumping solutions are encouraged to explore the benefits this innovative product brings to the marketplace.
High Efficiency End Suction Pumps: A Comprehensive Guide
End Suction Pump is one of the most essential and widely used tools in the industrial, commercial, and agricultural sectors. With its advanced technology and high performance, the End Suction Pump has become an integral part of various industries, providing efficient and reliable operations for numerous applications.The End Suction Pump is crafted with precision engineering and is designed to deliver high flow rates and low to medium head. It is highly efficient and cost-effective, making it the perfect choice for water supply, heating, cooling, and circulation systems. The pump is also widely used in irrigation, drainage, and fire protection systems, as well as in the chemical, petrochemical, and mining industries.One of the leading providers of End Suction Pumps is the renowned company {} which has been at the forefront of innovation and excellence in the pump industry for over three decades. With a strong focus on research and development, the company has continually pushed the boundaries of pump technology, delivering cutting-edge solutions to meet the evolving needs of its customers.{}'s End Suction Pump range is known for its superior performance, durability, and reliability. The pumps are designed to operate in the harshest of environments and under the most challenging conditions, ensuring uninterrupted operations for various applications. The company's commitment to quality and excellence has earned it a solid reputation in the industry, making it the go-to choice for businesses across the globe.The End Suction Pump from {} features a robust construction, with the use of high-quality materials and components that are built to last. The pumps are also equipped with advanced features such as efficient motor designs, precision-engineered impellers, and state-of-the-art controls, ensuring optimal performance and energy savings. With a wide range of sizes and configurations available, {} offers a comprehensive selection of End Suction Pumps to cater to the diverse needs of its customers.In addition to its exceptional product range, {} also prides itself on its customer-centric approach and comprehensive support services. The company's team of experts is dedicated to providing unparalleled technical assistance, maintenance, and repair services, ensuring that its customers can maximize the lifespan and performance of their End Suction Pumps. With a worldwide network of service centers and distributors, {} is able to deliver prompt and reliable support to its customers wherever they are located.Furthermore, {} is committed to sustainability and environmental responsibility, incorporating energy-efficient designs and eco-friendly materials in its End Suction Pumps. The company's focus on green initiatives and responsible manufacturing practices has not only reduced the environmental impact of its operations but has also helped its customers achieve their sustainability goals.Looking ahead, {} continues to lead the way in pump technology, with ongoing investments in research and development to further enhance its End Suction Pump range. The company is also actively expanding its global footprint, forging new partnerships and collaborations to bring its innovative solutions to a wider audience.With its unwavering commitment to excellence, innovation, and customer satisfaction, {} remains a trusted leader in the pump industry, delivering superior End Suction Pump solutions that set the standard for performance and reliability. As businesses and industries continue to evolve and grow, {} will undoubtedly remain at the forefront, providing the cutting-edge technology and support that its customers need to succeed.
Acid Submerged Pumps: Features, Applications, and Benefits
Certainly! Please provide the company introduction you'd like me to incorporate, and share the news content about Acid Submerged Pumps (without the brand name). Once I have that information, I’ll be able to draft the 800-word news article for you.
High-Efficiency Centrifugal Pump for Industrial Use
Din Ansi Centrifugal Pump, a leading provider of high-quality industrial pumps, has announced the launch of their latest innovative product. The new centrifugal pump, which is designed for various industrial applications, promises to deliver superior performance and reliability.With over 20 years of experience in the industry, Din Ansi Centrifugal Pump has established itself as a trusted name in the field of industrial pumps. The company is known for its commitment to quality, innovation, and customer satisfaction. Their team of experienced engineers and technical experts work tirelessly to develop cutting-edge pumping solutions that meet the needs of their diverse clientele.The new centrifugal pump is the result of extensive research and development efforts by Din Ansi Centrifugal Pump's team of experts. It is designed to offer high efficiency, low maintenance, and long-term reliability, making it an ideal choice for a wide range of industrial applications. The pump is built to withstand the toughest operating conditions and deliver consistent performance even in the most demanding environments.One of the key features of the new centrifugal pump is its advanced design, which maximizes energy efficiency and minimizes operational costs. This makes it an environmentally friendly and cost-effective solution for industrial pumping needs. In addition, the pump is equipped with state-of-the-art technology that ensures smooth and reliable operation, reducing the risk of downtime and maintenance issues.Furthermore, Din Ansi Centrifugal Pump's latest offering is backed by a comprehensive warranty and after-sales support, ensuring peace of mind for their customers. The company is committed to providing the highest level of service and support, and their team is always on hand to assist clients with any technical queries or concerns they may have."We are thrilled to introduce our latest centrifugal pump to the market," said a spokesperson for Din Ansi Centrifugal Pump. "This pump represents the culmination of our continuous efforts to develop cutting-edge pumping solutions that meet the evolving needs of our customers. We are confident that it will set new benchmarks for performance, reliability, and efficiency in the industry."Din Ansi Centrifugal Pump's commitment to quality and innovation has earned them a loyal customer base and a strong reputation in the industry. Their pumps are used in a wide range of industries, including oil and gas, petrochemical, chemical processing, water and wastewater treatment, and many others.The company's dedication to excellence extends beyond their products; they also prioritize sustainability and environmental responsibility in all aspects of their operations. Din Ansi Centrifugal Pump adheres to stringent quality and safety standards, ensuring that their pumps are manufactured and tested to the highest industry specifications.In conclusion, Din Ansi Centrifugal Pump's new centrifugal pump is poised to make a significant impact in the industrial pumping sector. With its innovative design, superior performance, and unwavering commitment to customer satisfaction, this pump represents another milestone in the company's continued success. As they continue to push the boundaries of pumping technology, Din Ansi Centrifugal Pump remains a driving force in the industry, setting new standards for excellence and reliability.
Sure! Please provide the original news content or title including the brand name, and I'll rewrite it for SEO without the brand name.
Certainly! Please provide the specific news content and the company introduction you'd like me to use. Once I have those details, I can craft an 800-word news article for you, ensuring that the brand name is removed as requested.