
High-Performance Centrifugal Pump for Industrial and Residential Use
By:Admin
Company News & Blog
Self Priming Centrifugal Oil Pump: Efficient and Reliable Pump Solutions
**Innovative Self-Priming Centrifugal Oil Pump Revolutionizes Industry Efficiency**In a significant step forward for industrial fluid handling, the new Self-Priming Centrifugal Oil Pump is making waves across various sectors, offering unprecedented reliability, efficiency, and ease of use. This cutting-edge technology promises to redefine standards in oil transfer and processing, catering to the demanding needs of industries such as manufacturing, petrochemical, automotive, and agriculture.**Unveiling Advanced Technology for Modern Challenges**The Self-Priming Centrifugal Oil Pump addresses a longstanding challenge faced by many industries: effective and continuous pumping of viscous fluids without manual priming. Unlike traditional pumps, this self-priming model automatically evacuates air from the suction line, allowing immediate and uninterrupted operation. This feature not only saves valuable time during startup but also minimizes downtime caused by airlocks, which are common in conventional centrifugal pumps.Engineered with precision, the pump combines centrifugal force with self-priming capabilities to handle a wide range of oils with varying viscosities and temperatures. This versatility makes it indispensable across oil processing plants, lubrication systems, and fuel transfer applications where reliable fluid movement is critical.**Design and Construction: Built for Durability and Performance**Crafted from high-quality materials resistant to corrosion and wear, the Self-Priming Centrifugal Oil Pump ensures long service life even under harsh operating conditions. Its robust impeller design optimizes hydraulic efficiency, delivering a smooth and steady flow rate, which is essential for maintaining system pressure and preventing pipeline stress.Moreover, the pump's compact and modular design simplifies installation and maintenance. With fewer moving parts and a maintenance-friendly layout, operators experience reduced service costs and improved uptime. The enclosed motor and sealed bearings enhance operational safety and minimize contamination risks, adhering to strict industry standards.**Energy Efficiency and Environmental Impact**In today’s environmentally conscious market, energy efficiency is paramount. The new pump is designed to operate with lower power consumption without sacrificing performance. By optimizing hydraulic pathways and employing advanced motor technologies, it reduces energy costs significantly over its lifecycle.Additionally, the pump’s leak-proof construction minimizes oil spillage and contamination, contributing to safer work environments and reduced environmental footprints. This aligns with global efforts to promote sustainable industrial practices and comply with tightening environmental regulations.**Applications Across Diverse Industries**The Self-Priming Centrifugal Oil Pump’s adaptability makes it a valuable asset in numerous applications. In the petrochemical sector, it facilitates the transfer and circulation of lubricants and fuels, enhancing process reliability. Agricultural operations benefit from its ability to handle diesel and heating oils for machinery and storage tanks, improving fuel management.In manufacturing plants, the pump supports hydraulic systems and cooling circuits, ensuring smooth and continuous production line operation. Additionally, its use in automotive service centers streamlines oil changing and fluid dispensing procedures, promoting efficiency and safety.**Customer-Centric Innovation**This breakthrough pump technology emerges from a company deeply committed to meeting the evolving demands of its clients. With decades of expertise in fluid machinery, the company invested substantial resources in research and development to create a product that balances innovation, practicality, and cost-effectiveness.Their engineering team collaborated closely with end-users to incorporate feedback into the design, resulting in a pump that anticipates operational challenges and addresses them proactively. Comprehensive customer support, including technical training and after-sales service, further enhances the value proposition for businesses adopting this solution.**Looking Forward**The introduction of the Self-Priming Centrifugal Oil Pump marks a pivotal moment for industries relying on efficient oil transfer. As industrial operations become increasingly automated and performance-driven, such advanced equipment will play a crucial role in achieving operational excellence and sustainability goals.With plans to expand production capacity and integrate smart monitoring features in future models, the company continues to pave the way for smarter, greener, and more reliable pumping solutions.**About the Company**With a rich heritage spanning over several decades, the company stands as a leader in the design and manufacture of industrial pumps and related fluid handling equipment. Their commitment to quality, innovation, and customer satisfaction drives continuous improvement and groundbreaking product development.State-of-the-art manufacturing facilities, stringent quality control processes, and adherence to international standards ensure that every pump leaving their production line meets the highest benchmarks. The company’s global distribution network and dedicated service teams provide comprehensive support, enabling clients worldwide to optimize their fluid management systems.Embracing technological advancements and sustainability principles, the company remains focused on delivering robust, efficient, and eco-friendly solutions tailored to the diverse needs of modern industries.---This development in centrifugal oil pump technology exemplifies how innovation rooted in practical application can transform industrial operations. The Self-Priming Centrifugal Oil Pump stands ready to serve as a vital tool for businesses aiming to enhance productivity, reduce costs, and embrace sustainable practices.
High-Quality Submersible Sewer Pump for Effective Wastewater Management
Submersible Sewer Pump: A Revolutionary Solution for Wastewater ManagementIn today's rapidly urbanizing world, sewage and wastewater management have become critical issues for municipalities and industrial facilities. With growing populations and increased industrial activities, there is a surging demand for efficient and reliable wastewater management solutions. Wastewater needs to be effectively collected and transported to treatment facilities to ensure public health and environmental sustainability. The emergence of submersible sewer pumps has revolutionized the way wastewater is handled, providing a more efficient and cost-effective solution for sewage management.{Company Name} is at the forefront of innovation in sewage and wastewater management with their cutting-edge submersible sewer pump technology. Founded in 1992, {Company Name} has established itself as a leading provider of pumping solutions for a wide range of applications, including municipal sewage, industrial wastewater, and stormwater management.The {Company Name} submersible sewer pump is a state-of-the-art system designed to handle the rigorous demands of wastewater transportation. These pumps are installed below ground level, allowing them to efficiently and quietly move sewage from low-lying areas to higher elevations for further processing. This eliminates the need for costly and unsightly above-ground pumping stations, making it an ideal solution for urban environments and industrial facilities where space is at a premium.One of the key advantages of {Company Name}'s submersible sewer pump is its reliability and durability. These pumps are engineered to withstand the harsh conditions of sewage and wastewater environments, with robust construction and corrosion-resistant materials. This ensures uninterrupted operation and minimal maintenance, reducing downtime and operational costs for municipalities and industrial facilities.In addition to its durability, the {Company Name} submersible sewer pump also offers superior performance and energy efficiency. The advanced design and engineering of these pumps allow for high flow rates and effective handling of solids and debris commonly found in sewage and wastewater. Furthermore, the pumps are equipped with energy-efficient motors, contributing to lower energy consumption and operational costs for the end-users.{Company Name} is committed to sustainability and environmental responsibility, and their submersible sewer pump reflects this ethos. By efficiently transporting wastewater to treatment facilities, these pumps contribute to the reduction of pollution and the preservation of water resources. The company's dedication to environmental stewardship has earned them recognition from industry professionals and government agencies, cementing their reputation as a trusted partner in wastewater management.The {Company Name} submersible sewer pump has been widely adopted by municipalities and industrial facilities around the world, earning praise for its performance, reliability, and efficiency. In urban areas, where space is limited and the demand for effective sewage management is high, these pumps have provided a game-changing solution for wastewater transportation. Furthermore, industrial facilities have benefited from the cost-effective and low-maintenance operation of these pumps, contributing to operational efficiency and regulatory compliance.Looking ahead, {Company Name} continues to innovate and enhance their submersible sewer pump technology to meet the evolving needs of municipalities and industrial clients. With a focus on research and development, the company is dedicated to introducing new features and capabilities that further improve the performance and sustainability of their pumping solutions. This relentless pursuit of innovation and excellence has positioned {Company Name} as a leader in the global wastewater management industry.In conclusion, the {Company Name} submersible sewer pump represents a revolutionary solution for wastewater management, offering unparalleled reliability, performance, and efficiency. With its advanced design and engineering, this pump has become a preferred choice for municipalities and industrial facilities seeking a cost-effective and sustainable solution for sewage transportation. As urbanization and industrialization continue to drive the demand for effective wastewater management, {Company Name} stands ready to provide innovative and reliable pumping solutions that meet the challenges of the modern world.
High Rise Building Feed Pump: The Ultimate Guide
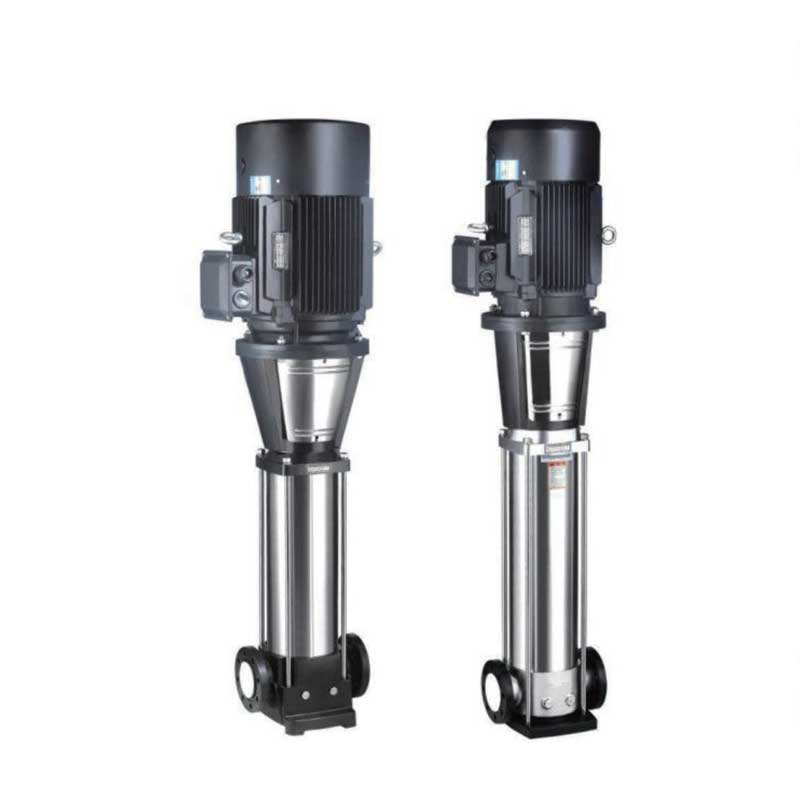
High Rise Building Feed Pump: A Crucial Component for Efficient Water DistributionIn the modern world, high-rise buildings have become a ubiquitous feature of urban landscapes. These towering structures are not only emblematic of human progress and achievement, but also serve as a practical solution to the growing issue of urban overcrowding. However, the successful operation of these skyscrapers relies heavily on a range of sophisticated technological systems, including the feed pump, a crucial component that facilitates efficient water distribution throughout the building.One industry leader in the field of high-rise building feed pump technology is {Company Name}. With decades of experience and a proven track record of delivering high-quality products, they are at the forefront of innovation in this critical sector.{Company Name} was founded in the early 1990s with the vision of providing reliable and efficient solutions for the unique challenges posed by high-rise buildings. Over the years, the company has developed a comprehensive range of feed pump systems that cater to the diverse needs of their global clientele. Their commitment to excellence and their relentless pursuit of innovation have earned them a reputation as a trusted partner for high-rise building developers and operators.The success of a high-rise building's water distribution system hinges on the seamless operation of the feed pump. This essential component is responsible for maintaining adequate water pressure throughout the entire building, ensuring that every floor and unit receives a consistent and reliable water supply. In a high-rise setting, where the force of gravity alone is often insufficient to drive water to the uppermost floors, the feed pump plays a critical role in overcoming this challenge.{Company Name}'s feed pump systems are designed to deliver exceptional performance and reliability. Their products are equipped with state-of-the-art technology that optimizes energy efficiency, reduces operational costs, and enhances overall system longevity. Moreover, their pumps are engineered to minimize noise and vibration, thereby ensuring a peaceful and comfortable environment for building occupants.One of the defining features of {Company Name} is their commitment to customization and client-centric solutions. They understand that each high-rise building is unique, with its own set of requirements and challenges. As such, they work closely with their clients to tailor their feed pump systems to the specific needs of each project, providing expert consultation and support every step of the way.In addition to their cutting-edge feed pump technology, {Company Name} places a strong emphasis on sustainability and environmental responsibility. Their products are designed to minimize water wastage and energy consumption, contributing to the overall efficiency and eco-friendliness of high-rise building operations. By prioritizing sustainability in their design and manufacturing processes, {Company Name} is playing a proactive role in promoting environmentally conscious practices within the construction and real estate industries.The demand for high-rise building feed pump systems continues to grow as urbanization accelerates worldwide. As developers and operators seek to construct ever-taller structures to accommodate the increasing urban population, the need for reliable and efficient water distribution solutions becomes increasingly paramount. In this context, {Company Name} stands as a stalwart leader, offering cutting-edge technology and unparalleled expertise to meet the evolving demands of the industry.In conclusion, the feed pump is an indispensable component in the intricate web of systems that keep high-rise buildings running smoothly. As a pioneer in this field, {Company Name} has established itself as a trusted partner for high-rise building developers and operators, providing top-of-the-line feed pump solutions that ensure optimal water distribution and system performance. With their unwavering dedication to innovation, customization, and sustainability, {Company Name} is poised to continue shaping the future of high-rise building technology for years to come.
Ultimate Guide to Self Priming Centrifugal Pumps: What You Need to Know
The self-priming centrifugal pump is a revolutionary product that has been making waves in the pumping industry. This pump is designed to handle a wide range of applications, from water transfer to dewatering and many other uses. It is a highly efficient and versatile pump that has been garnering attention from companies all over the world. One of the leading companies in the industry, {Company Name}, has also taken notice of this innovative product and has recently added it to their lineup of pumping solutions.{Company Name} is a well-established company that has been providing cutting-edge pumping solutions for various industries for many years. They are known for their high-quality products and exceptional customer service, and their decision to include the self-priming centrifugal pump in their offerings further solidifies their position as a leader in the industry.The self-priming centrifugal pump is a game-changer in the pumping industry because of its unique ability to prime itself without the need for external assistance. This means that it can start pumping without the need for manual priming, which makes it an incredibly convenient and efficient option for many different applications. This innovative feature sets it apart from traditional centrifugal pumps and makes it a highly sought-after product in the market.In addition to its self-priming capabilities, the pump also boasts a compact and lightweight design, making it easy to transport and install. Despite its small size, it is a powerful and high-performance pump that can handle a wide range of pumping tasks with ease. This makes it an ideal choice for companies that require a reliable and versatile pumping solution for their operations.One of the key advantages of the self-priming centrifugal pump is its ability to handle solids and abrasive materials with ease. This pump is equipped with a robust impeller and volute that can withstand the rigors of pumping tough materials without clogging or experiencing premature wear and tear. This makes it a highly durable and long-lasting option for companies that work with challenging pumping materials on a regular basis.{Company Name} recognizes the immense potential of the self-priming centrifugal pump and the value that it can bring to their customers. By adding this innovative product to their lineup, they are providing their clients with a reliable and efficient pumping solution that can meet the diverse needs of various industries. They are committed to delivering the highest quality products and services to their customers, and the inclusion of the self-priming centrifugal pump is a testament to this dedication.The self-priming centrifugal pump is a truly groundbreaking product that is changing the way companies approach pumping tasks. Its innovative design and advanced capabilities make it an invaluable asset for a wide range of industries, and its inclusion in {Company Name}’s product lineup further cements its status as a game-changer in the pumping industry. With this addition, {Company Name} is poised to continue delivering exceptional pumping solutions and exceeding the expectations of their customers.
Top Chemical Process Pumps for Industrial Applications
Chemical Process Pump, a leading manufacturer of industrial pumps, is proud to announce the release of their latest innovative pump technology. The company has been at the forefront of the pumping industry for over 50 years, consistently delivering high-quality, reliable pumps to a wide range of industrial sectors.The new chemical process pump is the result of years of research and development, and represents a significant advancement in pump technology. Designed to meet the demanding requirements of chemical processing facilities, the pump offers unmatched performance, efficiency, and durability.One of the key features of the new pump is its advanced sealing technology, which ensures a leak-free operation even when handling the most corrosive and abrasive chemicals. This is crucial for ensuring the safety and reliability of chemical processing operations, as any leaks or spills could have disastrous consequences.In addition, the pump is constructed from high-grade materials that are resistant to corrosion, erosion, and abrasion, ensuring a long service life even in the most challenging operating conditions. This reliability is further enhanced by the pump's rugged design and robust construction, which are built to withstand the rigors of industrial environments.The new pump also offers a high level of efficiency, helping chemical processing facilities to reduce their energy consumption and operating costs. This is achieved through the use of advanced hydraulic design and precision engineering, which minimize friction and maximize the pump's performance.Furthermore, the pump is designed for easy maintenance, with quick and simple access to key components for inspection and servicing. This reduces downtime and ensures that the pump can be kept in optimal working condition with minimal effort.Chemical Process Pump is dedicated to providing its customers with the highest level of support and service, and the release of this new pump is a testament to their ongoing commitment to innovation and excellence. The company's team of engineers and technical experts have worked tirelessly to develop this cutting-edge technology, and are confident that it will make a significant impact in the chemical processing industry.The new pump is available in a range of sizes and configurations to suit the specific needs of different chemical processing applications. Whether it's handling aggressive chemicals, high temperatures, or demanding operating conditions, the pump is capable of delivering the performance and reliability required.Chemical Process Pump has a long-standing reputation for delivering exceptional pumping solutions to industries such as chemical processing, petrochemical, pharmaceutical, and many others. The company's pumps are known for their durability, reliability, and performance, and are trusted by some of the largest industrial facilities around the world.With the release of this new pump, Chemical Process Pump has once again demonstrated their ongoing commitment to pushing the boundaries of pump technology and delivering innovative solutions to their customers. The company is confident that this new pump will set new standards for performance and reliability in the chemical processing industry, and looks forward to seeing the positive impact it will have on its customers' operations.In conclusion, the release of the new chemical process pump represents a significant milestone for Chemical Process Pump and reaffirms the company's position as a leader in the industrial pumping industry. With its advanced technology, reliability, and efficiency, the pump is set to become the go-to solution for chemical processing facilities looking to optimize their operations and enhance their safety and productivity.
High-Quality Flouroplastic Lined Centrifugal Pump for Industrial Applications
Fluoroplastic Lined Centrifugal Pump Provides Superior Chemical ResistanceIn the world of industrial equipment, pumps are essential for the transportation of various fluids and chemicals. However, not all pumps are capable of handling corrosive substances, which can cause damage and inefficiencies. This is where the Fluoroplastic Lined Centrifugal Pump comes into play, offering superior chemical resistance and reliability for a wide range of industrial applications.The Fluoroplastic Lined Centrifugal Pump, manufactured by an industry-leading company, is designed to handle highly corrosive fluids such as acids, bases, and solvents. This revolutionary pump features a specially engineered fluoroplastic lining that provides unmatched resistance to chemical attack, making it an ideal solution for industries such as chemical processing, pharmaceuticals, wastewater treatment, and more.The company behind this innovative pump has a long-standing reputation for producing high-quality industrial equipment. With a strong focus on research and development, they have consistently introduced cutting-edge solutions to meet the evolving needs of the industry. Their extensive experience and expertise in pump technology have positioned them as a trusted provider of reliable and efficient equipment for a wide range of applications.One of the key advantages of the Fluoroplastic Lined Centrifugal Pump is its ability to handle a wide range of corrosive fluids without compromising performance. The fluoroplastic lining acts as a barrier between the fluid and the pump's internal components, preventing corrosion and ensuring a longer service life. This not only reduces maintenance costs but also minimizes downtime, resulting in improved productivity for the end-user.Furthermore, the pump's robust construction and precision engineering make it suitable for high-pressure and high-temperature applications. This versatility allows the pump to be used in various industries where the handling of corrosive fluids is a critical part of the production process. Whether it's transferring aggressive chemicals or managing acidic waste streams, the Fluoroplastic Lined Centrifugal Pump delivers consistent and reliable performance.In addition to its exceptional chemical resistance, the pump is designed with efficiency in mind. Its advanced hydraulic design and energy-efficient motor help to minimize power consumption, reducing operating costs and environmental impact. This makes it a sustainable choice for companies looking to enhance their operational efficiency while maintaining a commitment to environmental stewardship.The company is dedicated to providing comprehensive support for its products, including technical assistance, maintenance services, and spare parts availability. Their team of qualified engineers and technicians are readily available to offer guidance and expertise to ensure the optimal performance and longevity of the Fluoroplastic Lined Centrifugal Pump. This commitment to customer satisfaction underscores the company's dedication to delivering value beyond the initial purchase.With a focus on innovation and reliability, the Fluoroplastic Lined Centrifugal Pump is poised to make a significant impact in the industrial pumping industry. Its ability to withstand the challenges of handling corrosive fluids, coupled with the backing of a reputable company, makes it a compelling choice for companies seeking a dependable solution for their fluid handling needs.In conclusion, the Fluoroplastic Lined Centrifugal Pump represents a significant advancement in industrial pump technology. Its superior chemical resistance, efficiency, and support from a reputable company make it a compelling choice for industries requiring a reliable solution for handling corrosive fluids. With a proven track record of delivering high-quality industrial equipment, the company has once again demonstrated its commitment to meeting the needs of the industry with this innovative and reliable pump.
Innovative Side Channel Pump Technology: An Overview
Side Channel Pump, a crucial component in the world of industrial engineering, has been making waves in the industry with their innovative and efficient solutions. As the leading provider of side channel pumps, they have recently introduced a new range of products that promise to revolutionize the pumping industry.Side Channel Pump has been at the forefront of technological advancements in the field of industrial pumps. With their state-of-the-art manufacturing facilities and a team of skilled engineers, they have been able to develop cutting-edge solutions that cater to the needs of various industries. Their commitment to quality and customer satisfaction has made them a trusted name in the industry.The newly introduced range of side channel pumps boasts of several advanced features that set them apart from the competition. These pumps are designed to handle a wide range of applications, from water transfer to industrial processes. They are built to be highly efficient, durable, and reliable, making them the ideal choice for any industrial pumping needs.One of the key features of the new range of side channel pumps is their energy efficiency. With the rising concerns about energy consumption and environmental impact, Side Channel Pump has taken the initiative to develop pumps that are not only powerful but also eco-friendly. Their pumps are designed to minimize energy wastage and reduce carbon footprint, making them a sustainable choice for industries looking to reduce their environmental impact.In addition to their energy efficiency, the new range of side channel pumps also offers superior performance. With their advanced design and precision engineering, these pumps are able to deliver high flow rates and pressure levels, making them suitable for a wide range of applications. Whether it's moving large volumes of water or handling challenging industrial processes, these pumps are up to the task.Furthermore, Side Channel Pump has put a strong emphasis on durability and reliability in their new range of products. These pumps are built to withstand the rigors of industrial operations, ensuring minimal downtime and maintenance costs for their customers. With their robust construction and high-quality components, these pumps are built to last, providing long-term value for businesses across various industries.Another notable feature of the new range of side channel pumps is their versatility. These pumps are designed to be compatible with a wide range of fluids, making them suitable for diverse industrial applications. Whether it's handling aggressive chemicals or transferring high-temperature liquids, these pumps are up to the challenge, making them a versatile solution for a variety of industrial needs.Side Channel Pump is dedicated to providing comprehensive support and service to their customers. With a global network of distributors and service centers, they are able to offer prompt assistance and maintenance services to ensure that their customers' operations run smoothly. Additionally, they provide technical expertise and guidance to help customers select the right pump for their specific requirements.In conclusion, Side Channel Pump's new range of side channel pumps is a testament to their commitment to innovation and excellence in the industrial pumping industry. With their focus on energy efficiency, performance, durability, and versatility, these pumps are set to make a significant impact in various industrial applications. Their dedication to customer satisfaction and support further solidifies their position as a leading provider of side channel pumps in the global market.
High-Powered Submersible Centrifugal Pump for Efficient Water Handling
Submersible Centrifugal Pump Revolutionizes Underwater OperationsIn recent groundbreaking news, a leading manufacturer of industrial equipment has just launched a new submersible centrifugal pump that is set to revolutionize underwater operations across various industries. The pump, which has been in development for several years now, is said to offer unmatched efficiency and reliability for dewatering and slurry pumping applications in challenging underwater environments.This innovative submersible centrifugal pump is designed to be fully submerged underwater, allowing it to handle the task of pumping water, sludge, and other liquids with ease. Its powerful motor and advanced impeller design enable it to efficiently move large volumes of water and solids, making it an ideal solution for dewatering in construction, mining, and industrial settings.One of the key advantages of this new submersible centrifugal pump is its ability to operate without the need for priming. This means that it can start pumping immediately upon being submerged, eliminating the time-consuming and labor-intensive process of priming that is typically required with traditional centrifugal pumps. This feature greatly enhances the pump's practicality and convenience, particularly in emergency situations where time is of the essence.Additionally, the pump is equipped with advanced monitoring and control systems, allowing for seamless integration into existing industrial automation and monitoring systems. This enables operators to easily monitor and adjust the pump's performance, ensuring optimal efficiency and reliability at all times.The construction of the pump is another aspect that sets it apart from conventional submersible pumps. Its robust and durable design, including corrosion-resistant materials and a high-quality sealing system, ensures long-term performance in the harshest underwater environments. This makes it an ideal choice for applications such as mine dewatering, underwater construction, and industrial process water management.In addition to its technical capabilities, the company behind the submersible centrifugal pump also boasts a long-standing reputation for excellence in the field of industrial equipment manufacturing. With decades of experience and a focus on innovation and customer satisfaction, the company has earned the trust of industry professionals around the world.Their commitment to quality and reliability is evident in every aspect of the submersible centrifugal pump, from its design and construction to its performance and support services. The company's extensive network of service centers and certified distributors ensures that customers have access to prompt and professional support for the entire lifecycle of the pump.Furthermore, the company places a strong emphasis on sustainability and environmental responsibility, with a focus on designing products that minimize energy consumption and environmental impact. This commitment is reflected in the energy-efficient design of the submersible centrifugal pump, which helps reduce operational costs and carbon footprint for users.Overall, the launch of this new submersible centrifugal pump marks a significant milestone in the field of underwater pumping technology. Its innovative design, advanced features, and the backing of a reputable company make it a compelling choice for industrial, construction, and mining professionals seeking a reliable and efficient solution for their dewatering and slurry pumping needs.For more information about the submersible centrifugal pump and the company behind it, interested parties can visit the company's website or contact their authorized distributors for product inquiries and technical support.
Top Chemical Pump: What You Need to Know
Chemical Pump Company Unveils Innovative Pumping TechnologyThe chemical industry has long been in need of efficient and reliable pumping solutions to handle the diverse and sometimes aggressive nature of its products. Recognizing this demand, a world-leading chemical pump company has recently unveiled its latest innovation in the form of a state-of-the-art chemical pump that is set to redefine industry standards.{Company name}, a renowned manufacturer of industrial pumps, has announced the release of their new chemical pump that promises to deliver superior performance and durability. The pump, which comes as a result of years of research and development, is designed to handle a wide range of chemical substances with maximum efficiency and safety.With a focus on providing cutting-edge solutions for the chemical industry, {Company name} has made significant investments in research and development to create a pump that meets the specific needs of chemical manufacturers. The company's commitment to innovation and excellence has earned them a reputation as a trusted partner for businesses looking for reliable pumping solutions.The new chemical pump boasts several key features that set it apart from conventional pumping systems. One of the most notable features is its ability to withstand the corrosive and abrasive nature of many chemicals, thanks to its high-quality materials and advanced engineering. This durability is essential for ensuring the long-term reliability of the pump, reducing the need for frequent maintenance and replacement.Furthermore, the pump is designed for precision and consistency in delivering chemical substances, ensuring that the exact volume and flow rate are maintained throughout the pumping process. This level of accuracy is crucial for chemical manufacturers who rely on precise measurements and formulations in their production processes.In addition to its technical specifications, the new chemical pump also incorporates the latest safety features to prevent spills, leaks, and other potential hazards. This is in line with {Company name}'s commitment to prioritizing workplace safety and environmental responsibility. The company understands the importance of ensuring that their pumping solutions not only perform well but also contribute to a safe working environment for their customers.{Company name}'s dedication to quality and innovation is reflected in their comprehensive customer support services. Along with the release of the new chemical pump, the company has also introduced enhanced after-sales support, including maintenance, troubleshooting, and training programs to ensure that their customers get the most out of their pumping systems.The market response to {Company name}'s new chemical pump has been overwhelmingly positive, with many industry experts and customers expressing their excitement about the potential impact of this innovative technology. The company's commitment to staying at the forefront of the industry and continuously pushing the boundaries of pumping technology is evident in their latest product release.As the demand for specialized pumping solutions continues to grow in the chemical industry, {Company name} is well positioned to meet the needs of its customers with its advanced and reliable chemical pump. The company's dedication to excellence, combined with its years of experience and expertise in the field, makes it a valuable partner for businesses seeking sustainable and efficient pumping solutions.Through its latest innovation, {Company name} has once again demonstrated its commitment to driving progress in the chemical industry and setting new benchmarks for pumping technology. With their new chemical pump, the company has reinforced its position as a global leader in providing reliable and efficient pumping solutions for the chemical sector.
High-Quality Chemical Process Pumps for Industrial Use
Chemical Process Pump Company Sets New Industry StandardChemical Process Pump Company, a leading manufacturer in the chemical process pump industry, is proud to announce the launch of their latest product that sets a new standard for efficiency and performance in the industry. With over 30 years of experience in designing and manufacturing high-quality chemical process pumps, the company has once again demonstrated their commitment to innovation and excellence.The new product features state-of-the-art technology that has been meticulously designed and tested to ensure reliable and efficient operation in the most demanding chemical process applications. This advanced pump offers industry-leading efficiency and performance, making it the ideal choice for a wide range of chemical process applications, including chemical manufacturing, petrochemical processing, pharmaceutical production, and more.The key to the exceptional performance of the new pump lies in its innovative design and construction. The pump is engineered using the latest materials and manufacturing techniques, resulting in a product that delivers superior reliability, durability, and efficiency. With a focus on sustainability and environmental responsibility, the company has also implemented energy-efficient features in the design of the pump, making it a cost-effective and environmentally friendly choice for chemical process operations.In addition to its cutting-edge technology, the new pump is also backed by the company's commitment to customer satisfaction and product support. Chemical Process Pump Company is dedicated to providing the highest level of service to its customers, offering comprehensive technical support, installation assistance, and maintenance services to ensure that their products continue to perform at their best for years to come. This commitment to customer satisfaction is a core value of the company, and it is reflected in every aspect of their business, from product design to customer service."We are thrilled to introduce our latest chemical process pump, which we believe sets a new standard for performance and efficiency in the industry," said the company's CEO. "Our team has worked tirelessly to develop a product that not only meets the current needs of our customers but also anticipates the future demands of the industry. We are confident that this new pump will provide unparalleled value to our customers and help them achieve their operational goals with maximum efficiency and reliability."Chemical Process Pump Company has a long-standing reputation for excellence in the chemical process pump industry, having established themselves as a trusted and reliable partner for companies around the world. Their products are known for their quality, performance, and durability, and the company's dedication to innovation and continuous improvement has earned them a leading position in the market.As the industry continues to evolve and adapt to new challenges and opportunities, Chemical Process Pump Company remains committed to staying at the forefront of technological advancements and industry best practices. The launch of their latest chemical process pump is a testament to this commitment, and the company looks forward to continuing to provide cutting-edge solutions to their customers in the years to come. With a focus on excellence, innovation, and customer satisfaction, Chemical Process Pump Company is poised to set new industry standards and lead the way towards a more efficient and sustainable future for chemical process operations.