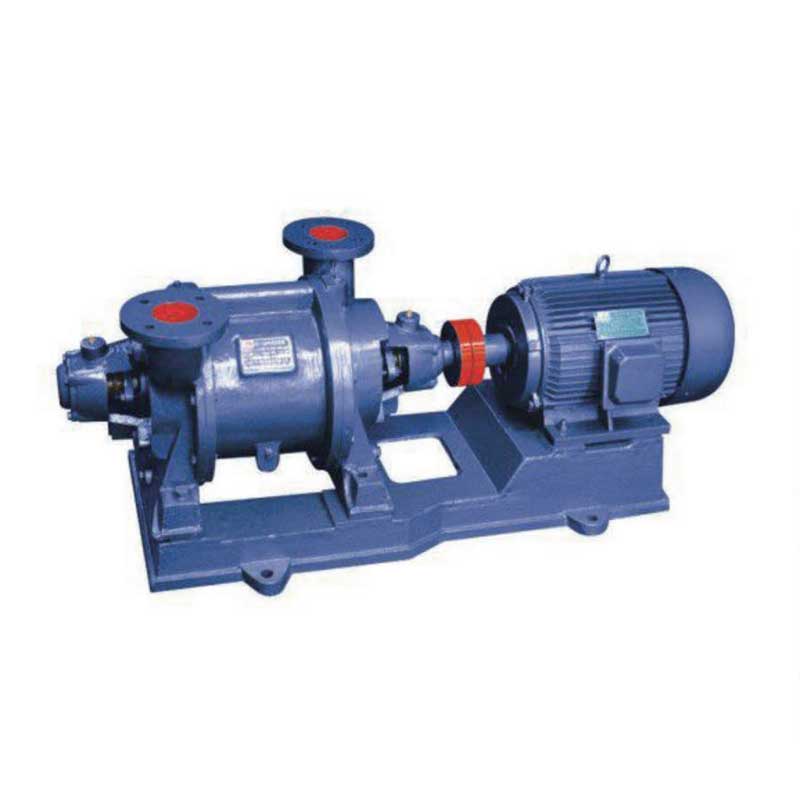
High-Quality Chemical Process Pumps for Efficient Industrial Applications
Certainly! Please provide the specific news content about the Chemical Process Pump and the company introduction you’d like me to incorporate. Once I have those details, I can craft an 800-word news article for you.
Read More
Top-rated Immersible Pump Factory Offers Quality Products for Water Applications
Fy Immersible Pump Factory, a leading manufacturer of immersible pumps, has been making waves in the industry with its high-quality products and innovative solutions. The company has been a pioneer in the field of immersible pumps and has been serving a wide range of industries including agriculture, mining, construction, and municipal applications.Established in [year], Fy Immersible Pump Factory has always been committed to providing the best products and services to its customers. With a strong focus on research and development, the company has continuously strived to improve its products and introduce new technologies to meet the evolving needs of the market.One of the key strengths of Fy Immersible Pump Factory is its state-of-the-art manufacturing facility, which is equipped with the latest machinery and equipment. This allows the company to produce a wide range of immersible pumps that are known for their durability, efficiency, and performance. The company also has a team of highly skilled engineers and technicians who ensure that every product that leaves the factory meets the highest quality standards.In addition to its manufacturing capabilities, Fy Immersible Pump Factory also has a strong focus on customer satisfaction. The company has a dedicated team of customer service representatives who work closely with clients to understand their specific requirements and provide them with customized solutions. This customer-centric approach has helped the company build strong and long-lasting relationships with its clients, who continue to trust Fy Immersible Pump Factory for all their immersible pump needs.Furthermore, Fy Immersible Pump Factory is committed to environmental sustainability and has implemented various measures to reduce its carbon footprint. The company has invested in eco-friendly technologies and processes to ensure that its operations have minimal impact on the environment. This commitment to sustainability has not only helped the company become a responsible corporate citizen but has also garnered it a positive reputation in the industry.Another important aspect of Fy Immersible Pump Factory's success is its global reach. The company has a strong presence in international markets and has an extensive distribution network that allows it to reach customers across the globe. This global footprint has helped Fy Immersible Pump Factory establish itself as a trustworthy and reliable supplier of immersible pumps to a wide range of industries worldwide.Looking ahead, Fy Immersible Pump Factory is focused on continued innovation and expansion. The company is constantly investing in research and development to stay ahead of the curve and introduce new products that cater to the ever-changing needs of the market. Additionally, Fy Immersible Pump Factory is looking to expand its presence in new markets and reach out to more customers around the world.In conclusion, Fy Immersible Pump Factory has established itself as a leader in the immersible pump industry, thanks to its commitment to quality, innovation, customer satisfaction, and sustainability. With its strong manufacturing capabilities, dedicated team, and global reach, the company is well-positioned for continued success in the years to come.
Read More
High-quality Petrochemical Flow Pump for Efficient Operations
Petrochemical Flow Pump, a leading company in the manufacturing and distribution of high-quality pumping solutions for the petrochemical industry, has announced the release of its latest innovative pump technology. The new pump is designed to meet the growing demands of the petrochemical industry, providing efficient and reliable performance in the transfer of various chemicals and petrochemical products.The company, with a strong commitment to research and development, has a long history of producing robust and durable pumps that are specifically tailored to the unique requirements of the petrochemical sector. With a focus on precision engineering and cutting-edge technology, Petrochemical Flow Pump has established itself as a trusted and preferred supplier for many petrochemical companies around the world.The new pump features advanced design and construction, incorporating the latest materials and engineering techniques to ensure optimal performance and durability. It is capable of handling a wide range of chemicals, including corrosive and abrasive fluids, at high temperatures and pressures, making it ideal for the rigorous demands of petrochemical processing.One of the key features of the new pump is its adaptability to a variety of petrochemical applications, including the transfer of crude oil, refined products, and specialty chemicals. Its robust construction and high-efficiency impeller design enable it to maintain consistent flow rates and pressure levels, contributing to the overall efficiency and reliability of petrochemical processes.In addition to its exceptional performance, the new pump also incorporates advanced safety features to ensure the protection of personnel and equipment. With a focus on compliance with industry standards and regulations, Petrochemical Flow Pump has integrated state-of-the-art safety mechanisms into the pump's design, providing peace of mind for operators and managers in petrochemical facilities.Furthermore, the company's commitment to sustainability is evident in the energy-efficient design of the new pump, contributing to reduced environmental impact and operational costs for petrochemical companies. By leveraging innovative technologies and sustainable practices, Petrochemical Flow Pump continues to lead the way in promoting environmental responsibility within the petrochemical industry.With a global network of sales and service centers, Petrochemical Flow Pump is well-positioned to deliver its latest pump technology to petrochemical companies worldwide. The company's team of experienced engineers and technical experts provide comprehensive support and assistance, ensuring seamless integration and operation of the new pump within existing petrochemical systems.As part of its dedication to customer satisfaction, Petrochemical Flow Pump offers customized solutions and personalized support to meet the specific needs of each petrochemical operation. Whether it's a small-scale facility or a large petrochemical complex, the company is committed to providing reliable pumping solutions that enhance productivity and operational efficiency.In conclusion, Petrochemical Flow Pump's latest pump technology represents a significant advancement in the petrochemical industry, offering unmatched performance, safety, and sustainability. With a proven track record of delivering high-quality pumping solutions, the company continues to be a trusted partner for petrochemical companies seeking to optimize their processes and achieve their operational goals. As the demand for reliable and efficient pumping solutions in the petrochemical sector continues to grow, Petrochemical Flow Pump remains at the forefront, driving innovation and setting new standards for excellence in the industry.
Read More
Durable Sludge Pumps for Heavy Duty Applications
Heavy Duty Sludge Pumps – A Key Component in Efficient Industrial OperationsIn the world of industrial operations, the effective management of sludge and waste materials is crucial for ensuring smooth and efficient processes. And when it comes to moving and disposing of heavy sludge, having the right equipment is absolutely essential.This is where the Heavy Duty Sludge Pumps from {Company Name} come into play. With their unparalleled performance and reliability, these pumps have become a key component in numerous industrial operations around the world. Let's take a closer look at these remarkable pumps and the company behind them.{Company Name} is a globally renowned manufacturer of heavy-duty industrial pumps and equipment. With a legacy spanning several decades, the company has earned a reputation for delivering high-quality, innovative solutions for a wide range of industrial applications. From mining and construction to wastewater management and environmental remediation, {Company Name} products have proven their value in diverse industries.At the heart of {Company Name}'s product lineup are their Heavy Duty Sludge Pumps. These robust pumps are specifically designed to handle the toughest sludge and waste materials with ease. Featuring a combination of high-capacity pumping capabilities and durable construction, these pumps are capable of delivering consistent performance in the most demanding environments.One of the key features of {Company Name}'s Heavy Duty Sludge Pumps is their exceptional reliability. Industrial operations rely heavily on consistent and uninterrupted processes, and these pumps are built to deliver exactly that. With minimal downtime and maintenance requirements, these pumps help businesses minimize costly disruptions and maximize their operational efficiency.Furthermore, {Company Name}'s Heavy Duty Sludge Pumps are designed for easy integration into existing systems. Whether it's in a mining operation, a wastewater treatment plant, or a construction site, these pumps can be seamlessly incorporated into various processes to streamline the handling and disposal of sludge. This level of flexibility makes them an ideal choice for businesses looking to optimize their operations without the need for extensive reconfiguration.In addition to their superior performance and reliability, {Company Name}'s Heavy Duty Sludge Pumps are also designed with environmental considerations in mind. These pumps are equipped with advanced features to minimize the impact on the environment, such as efficient energy consumption and emissions reduction. This not only helps businesses meet their sustainability goals but also contributes to a cleaner and healthier planet.Another distinguishing factor of {Company Name}'s Heavy Duty Sludge Pumps is the company's commitment to customer support and service. With a global network of service centers and a team of experienced professionals, {Company Name} is dedicated to ensuring that its customers receive the support they need, whenever they need it. This level of dedication to customer satisfaction sets {Company Name} apart from its competitors and gives businesses peace of mind when investing in their products.Looking ahead, {Company Name} continues to innovate and expand its product offerings to meet the evolving needs of the industrial sector. With a focus on research and development, the company is constantly exploring new technologies and design concepts to further enhance the performance and capabilities of its pumps.In conclusion, {Company Name}'s Heavy Duty Sludge Pumps are an indispensable asset for industrial operations that require efficient and reliable sludge handling solutions. With their exceptional performance, durability, and environmental consciousness, these pumps have proven themselves as a vital component in the success of businesses around the world. As {Company Name} continues to lead the way in pump manufacturing, the future looks bright for industries seeking to optimize their operations and minimize their environmental impact.
Read More
Efficient and Compact Short Setting Pump for Various Applications
Short Setting Pump Technology Revolutionizes the Pump IndustryIn recent years, the pump industry has seen a significant revolution in technology, and one of the leading innovations has been the development of short setting pump technology. This groundbreaking technology has been making waves in the industry, and one company at the forefront of this innovation is {COMPANY NAME}.{COMPANY NAME} is a global leader in the pump industry, with a rich history of innovation and a strong commitment to engineering excellence. The company has been at the forefront of developing cutting-edge pump technologies, and the introduction of short setting pump technology is a testament to their dedication to pushing the boundaries of what is possible in the industry.Short setting pump technology is a game-changer in the pump industry, offering significant advantages over traditional pump systems. The technology is designed to reduce the distance between the pump and the source of liquid, resulting in improved efficiency, reduced energy consumption, and lower operating costs. This innovation has the potential to revolutionize the way pumps are used across a wide range of industries, including oil and gas, water treatment, and manufacturing.One of the key benefits of short setting pump technology is its ability to improve the overall performance of pumping systems. By reducing the distance between the pump and the liquid source, the technology minimizes friction losses and pressure drops, resulting in improved flow rates and lower energy consumption. This not only leads to cost savings for businesses but also reduces the environmental impact of pumping operations.Another advantage of short setting pump technology is its versatility. This innovative technology can be applied to a wide range of pump designs, including centrifugal, positive displacement, and submersible pumps. This means that businesses across various industries can benefit from the advantages offered by short setting pump technology, regardless of their specific pumping needs.{COMPANY NAME} has been at the forefront of developing and commercializing short setting pump technology, and their efforts have not gone unnoticed. The company has received widespread recognition for their innovative approach to pump design and has garnered a reputation as a leading provider of cutting-edge pumping solutions.In a recent statement, {COMPANY NAME} CEO emphasized the importance of short setting pump technology in the pump industry, stating, "Our goal has always been to push the boundaries of what is possible in pump design and engineering. Short setting pump technology is a game-changer that has the potential to revolutionize the industry, and we are proud to be at the forefront of this innovation."The company's commitment to innovation and excellence has positioned them as a key player in the pump industry, and their focus on developing and commercializing short setting pump technology has solidified their reputation as a leader in the field. As the demand for more efficient and cost-effective pumping solutions continues to grow, it is clear that short setting pump technology will play a crucial role in shaping the future of the industry.In conclusion, short setting pump technology has the potential to revolutionize the pump industry, and {COMPANY NAME} is at the forefront of this exciting innovation. With its ability to improve pump performance, reduce energy consumption, and lower operating costs, short setting pump technology is set to become the new standard in pumping solutions. As the industry continues to evolve, it is clear that {COMPANY NAME} will remain a key player in driving this technological revolution forward.
Read More
Alloy Fluoroplastic Pump for High-performance Industrial Applications
FSB-L Alloy Fluoroplastic Pump: A Revolutionary Solution for Corrosive and Abrasive FluidsIn the world of industrial manufacturing and processing, the handling of corrosive and abrasive fluids poses some of the most significant challenges. Traditional pumps are often not suitable for these demanding applications, leading to frequent breakdowns, high maintenance costs, and operational inefficiencies. However, with the introduction of the FSB-L Alloy Fluoroplastic Pump by a leading pump manufacturer, a revolutionary solution has emerged to tackle these critical issues.The FSB-L Alloy Fluoroplastic Pump is specially designed to handle a wide range of corrosive and abrasive fluids such as acids, alkalis, solvents, and chemical mixtures. Its unique construction features a combination of alloy and fluoroplastic materials, making it highly resistant to chemical corrosion and wear. This innovative design ensures exceptional durability and long-term performance, even in the harshest industrial environments.One of the key advantages of the FSB-L Alloy Fluoroplastic Pump is its versatility. It can be used in various industries, including chemical processing, pharmaceuticals, wastewater treatment, and metal plating, among others. Its ability to handle a diverse range of fluids makes it an ideal choice for many different applications, providing significant value and efficiency to a wide array of operations.Moreover, the FSB-L Alloy Fluoroplastic Pump is equipped with advanced sealing and impeller designs that minimize the risk of leakage and enhance operational safety. This is particularly crucial when dealing with hazardous or toxic fluids, where containment is of utmost importance. The pump's reliable and leak-free performance ensures a secure working environment and compliance with stringent safety regulations.With the growing focus on environmental sustainability, the FSB-L Alloy Fluoroplastic Pump also offers significant benefits in terms of energy efficiency and reduced environmental impact. Its optimized hydraulic design and high-performance motor result in lower power consumption, contributing to overall energy savings and operational cost reduction. Additionally, its durable construction and minimal maintenance requirements contribute to a lower carbon footprint, making it a sustainable choice for conscientious businesses.The manufacturer behind the FSB-L Alloy Fluoroplastic Pump has a strong track record of delivering high-quality pumping solutions to the market. With decades of experience in pump design and engineering, the company has earned a reputation for innovation, reliability, and customer satisfaction. Its commitment to continuous improvement and technological advancement is reflected in the development of the FSB-L Alloy Fluoroplastic Pump, which sets a new standard for performance and reliability in the industry.In addition to its exceptional product quality, the company also places a strong emphasis on customer support and service. From initial consultation and pump selection to installation, commissioning, and after-sales maintenance, the manufacturer provides comprehensive support to ensure the seamless integration and operation of the FSB-L Alloy Fluoroplastic Pump. This commitment to customer satisfaction has established long-lasting partnerships with clients worldwide, who value the manufacturer as a trusted and dependable supplier of pumping solutions.The introduction of the FSB-L Alloy Fluoroplastic Pump represents a significant milestone in the pumping industry, offering a groundbreaking solution to the challenges of handling corrosive and abrasive fluids. Its advanced design, exceptional performance, and environmental sustainability make it a compelling choice for diverse industrial applications. Coupled with the manufacturer's expertise and dedication to customer satisfaction, the FSB-L Alloy Fluoroplastic Pump is poised to make a lasting impact in the global market, providing reliable and efficient pumping solutions for years to come.
Read More
Acid Submerged Pumps: Key Features and Applications
Certainly! Please provide the full news content about Acid Submerged Pumps and the company introduction you'd like me to use. Once I have those details, I will draft an 800-word news article for you without including any brand names.
Read More
Highly Efficient Self Priming Centrifugal Pump for Industrial Use
Self-Priming Centrifugal Pump Revolutionizes Industry StandardsIn today's rapidly evolving business landscape, companies are constantly seeking innovative solutions to improve their operations and increase efficiency. One such breakthrough in the world of industrial equipment is the introduction of the self-priming centrifugal pump, which has reshaped the industry standard for pump technology.Traditionally, centrifugal pumps require manual priming to remove air from the system before they can effectively move fluid. This process can be time-consuming and labor-intensive, leading to operational delays and increased costs. However, the self-priming centrifugal pump, pioneered by {company name}, has eliminated the need for manual priming, revolutionizing the way companies approach fluid transfer and management.The self-priming centrifugal pump is designed to automatically remove air from the system, allowing for quick and seamless operation without the need for manual intervention. This groundbreaking technology has significantly reduced the time and effort required to start and maintain centrifugal pumps, providing companies with a more efficient and cost-effective solution for their fluid transfer needs.{Company name}, a leading manufacturer of industrial equipment, has been at the forefront of this technological advancement. With a strong commitment to innovation and customer satisfaction, {company name} has dedicated substantial resources to the research and development of the self-priming centrifugal pump, resulting in a product that has set a new standard for performance and reliability in the industry.The self-priming centrifugal pump from {company name} has been widely adopted across various sectors, including manufacturing, agriculture, construction, and water treatment. Its ability to quickly and effectively move fluids, including water, chemicals, and wastewater, has made it a valuable asset for companies looking to streamline their operations and improve productivity.One of the key features of the self-priming centrifugal pump is its versatility and ease of use. With a simplified priming process and reduced maintenance requirements, the pump offers a user-friendly solution for a wide range of fluid transfer applications. This has made it an attractive choice for businesses of all sizes, from small-scale operations to large industrial facilities.Moreover, the self-priming centrifugal pump from {company name} is also known for its robust construction and durable performance, ensuring reliable operation even in the harshest of environments. This level of dependability has instilled confidence in customers, who have come to rely on the pump for their critical fluid transfer needs.In addition to its technological advancement, {company name} has also prioritized environmental sustainability in the design and production of the self-priming centrifugal pump. By incorporating energy-efficient features and eco-friendly materials, the company has demonstrated its commitment to reducing the environmental impact of its products, aligning with the growing demand for sustainable solutions in the industry.As the market continues to embrace the benefits of the self-priming centrifugal pump, {company name} remains dedicated to further enhancing its capabilities and exploring new applications for this game-changing technology. With a focus on continuous improvement and customer-driven innovation, {company name} is poised to lead the evolution of fluid transfer solutions for years to come.In conclusion, the introduction of the self-priming centrifugal pump has marked a significant advancement in industrial pump technology, setting a new standard for efficiency, reliability, and sustainability. With {company name} at the forefront of this innovation, businesses across various sectors can now benefit from a more streamlined and cost-effective solution for their fluid transfer needs, paving the way for a brighter and more efficient future in the industry.
Read More
High-Performance Pneumatic Diaphragm Pump for Efficient Fluid Transfer
Certainly! Please provide the news content about the Pneumatic Diaphragm Pump (without the brand name) and the company introduction, and I will craft an 800-word news article for you.
Read More
Hydraulic Transfer Pump: Efficient Fluid Handling Solutions
**Innovative Hydraulic Transfer Pump Revolutionizes Fluid Handling Solutions**In the ever-evolving landscape of industrial fluid management, the introduction of the latest Hydraulic Transfer Pump marks a significant milestone. Designed to enhance efficiency, reliability, and safety, this state-of-the-art pump is set to transform operations across multiple sectors including agriculture, chemical processing, and manufacturing.**Advanced Technology Meets Practical Design**The Hydraulic Transfer Pump stands out due to its robust engineering and user-centric design. Engineered to handle a wide range of fluids—from water and fuels to aggressive chemicals—this pump offers unparalleled versatility. Its hydraulic-driven mechanism ensures consistent power delivery even in challenging environments where electrical options may pose risks or limitations.One of the core advantages of this pump lies in its ability to operate seamlessly without direct electrical input, thus reducing the chance of sparks or electrical hazards. This feature is particularly crucial in volatile settings such as oil fields and chemical plants where safety cannot be compromised. Moreover, the pump’s design incorporates corrosion-resistant materials, extending its lifespan and reducing maintenance downtime.**Boosting Operational Efficiency**In industries where time and resource management are critical, the Hydraulic Transfer Pump delivers impressive performance metrics. With high flow rates and pressure capabilities, it accelerates transfer processes, enabling businesses to meet tight deadlines and maximize throughput. The pump’s simple yet effective hydraulic drive mechanism also minimizes energy consumption compared to traditional electric pumps, contributing to cost savings and sustainability goals.Additionally, the pump’s modular construction allows for easy integration into existing systems, granting companies the flexibility to upgrade their infrastructure without extensive overhauls. This adaptability makes it an attractive investment not only for new projects but also for retrofitting older facilities.**Company Introduction**Founded with a commitment to innovation and quality, the company behind this cutting-edge Hydraulic Transfer Pump has consistently pushed the boundaries of fluid technology. With decades of experience, the organization specializes in designing and manufacturing equipment that meets the highest industry standards. Their comprehensive portfolio spans pumps, mixers, and filtration systems tailored to diverse industrial applications.The company prides itself on a customer-centric approach, offering customized solutions and hands-on support. Their R&D team works closely with clients to develop products that address specific operational challenges, ensuring reliability and efficiency. Through continuous improvement and adherence to stringent quality controls, the company has established itself as a trusted partner worldwide.**Applications Across Industries**The versatility of the Hydraulic Transfer Pump makes it suitable for numerous applications:- **Agriculture:** Efficient irrigation water transfer, fertilizer and pesticide handling without risk of contamination.- **Chemical Processing:** Safe movement of corrosive or flammable liquids with reduced chance of leaks or spills.- **Oil and Gas:** Transfer of fuels and lubricants onsite, avoiding electrical hazards in explosive environments.- **Manufacturing:** Handling process fluids, coolants, and cleaning agents with minimal maintenance requirements.This broad applicability not only highlights the pump’s technical advantages but also its contribution to operational safety and environmental protection.**Commitment to Sustainability**Understanding the growing importance of sustainable operations, the company incorporates eco-friendly principles into product design. The hydraulic nature of the pump minimizes electrical use and burnouts, leading to lower energy demands. Furthermore, the use of durable materials reduces waste and replacement frequency.By supporting efficient fluid transfer processes, the pump helps reduce emissions related to fuel transfers and chemical leaks. This aligns with global efforts to promote greener industrial practices.**Customer Success Stories**Several clients have already reported transformative results after integrating the Hydraulic Transfer Pump into their workflows. One agricultural cooperative noted a 30% reduction in water transfer time, translating to increased crop yields and lower labor costs. A chemical processing plant highlighted improved safety records, attributing fewer incidents to the pump’s non-electrical operation and leak-resistant design.Such feedback reflects the tangible benefits and reliability the product offers, reinforcing its market position.**Future Prospects and Innovations**Looking ahead, the company continues to invest in research and development aimed at enhancing pump efficiency and expanding capabilities. Plans include smart monitoring systems that provide real-time performance data and predictive maintenance alerts, further minimizing downtime and operational risks.The company’s vision centers on delivering fluid handling solutions that not only meet but exceed customer expectations, adapting to evolving industrial challenges and technological advancements.**Conclusion**The introduction of this Hydraulic Transfer Pump represents a leap forward in fluid management technology. Its innovative hydraulic drive system, combined with durable construction and versatile applications, addresses key industry needs for safety, efficiency, and sustainability. Backed by a company renowned for excellence and customer focus, this pump is poised to become an essential tool across sectors demanding reliable fluid transfer solutions.As industries strive towards more efficient and safer operations, embracing such advanced equipment is a strategic step toward achieving long-term productivity and environmental goals. The Hydraulic Transfer Pump is not just a piece of machinery—it is a catalyst for enhanced industrial performance worldwide.
Read More